Best China PSC Tool Holder Manufacturer Supplier?
Choosing the Best China Psc Tool Holder Manufacturer Supplier requires more than comparing prices or polished catalog photographs. A PSC Tool Holder connects the machine spindle, cutting tool, and workpiece. Small errors can become visible chatter, uneven surfaces, or premature insert wear. Experienced buyers therefore examine runout, taper accuracy, balancing quality, clamping force, material consistency, and inspection records.
Dr. Tony Schmitz, a recognized machining dynamics researcher, has said, “The toolholder is the interface between the spindle and the cutting tool.” This simple statement deserves attention. A reliable supplier should explain how each holder is heat-treated, ground, measured, and tested. Ask for actual tolerance data, not only general promises. Check whether the manufacturer supports ISO 26623 compatibility and provides clear dimensional drawings. Confirm the available PSC sizes, pull-stud requirements, coolant options, and delivery capacity. These details matter on a busy shop floor, where a holder may run for hours beside hot chips and cutting fluid.
China has many capable PSC Tool Holder manufacturers, but quality is not automatically uniform. Some suppliers offer excellent machining and responsive technical support. Others may provide attractive samples without stable batch control. That weakness can be missed at first. It should not be ignored. A practical evaluation may include sample inspection, test cutting, repeatability checks, and communication with the engineering team. The best supplier is not always the cheapest one. It is the partner that documents performance, admits limitations, and improves when feedback exposes a problem. That is a less perfect, but more trustworthy, way to choose.
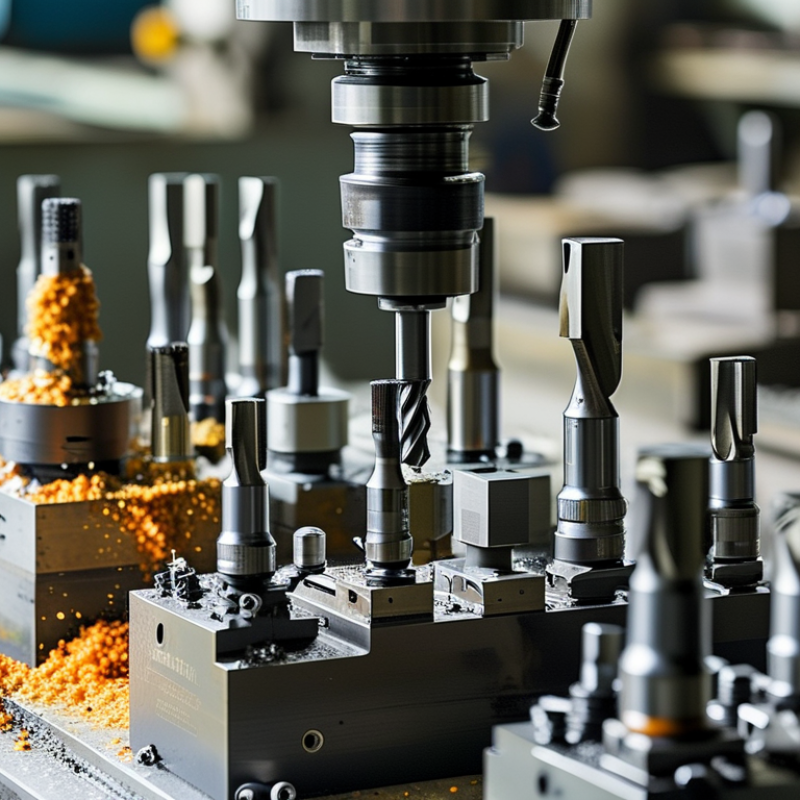
What Is a PSC Tool Holder? ISO 26623, Polygonal Shanks, and 1:20 Taper
Choosing the best China PSC tool holder manufacturer requires more than comparing prices. Understanding the standard comes first. PSC means Polygonal Shank with a conical taper. The holder locates against both surfaces, improving radial repeatability and axial positioning. ISO 26623 defines the interface dimensions, gauge requirements, and functional tolerances.
The taper is commonly 1:20, so the angle is shallow and stable during heavy cutting. The polygonal shank transfers torque through several contact faces, rather than relying on friction alone. In practical machining, this can reduce vibration and improve tool life. However, performance depends on accuracy. A poorly ground polygon can still create runout, even when the design is correct. That detail is easy to miss.
A reliable supplier should provide inspection records for taper size, polygon profile, concentricity, and surface finish. Ask how the holder is heat-treated and balanced. High-speed machining needs controlled balance, not vague claims. Check the pull-in force and verify compatibility with the spindle interface. Coolant delivery also matters, especially around the flange and cutting edge.
Small details matter. A clean gauge line matters. I would request sample measurement data before placing a large order. In one evaluation, a slight burr on the locating face caused inconsistent tool length. It was simple, but costly. The supplier should respond clearly, correct defects, and explain inspection methods. That practical transparency is often more valuable than a polished catalog.
Best China PSC Tool Holder Manufacturer Supplier? - What Is a PSC Tool Holder? ISO 26623, Polygonal Shanks, and 1:20 Taper
| Technical Dimension | Verified Information | Why It Matters When Selecting a Supplier |
|---|---|---|
| Definition | PSC means Polygon Shank Coupling. A PSC tool holder uses a polygonal taper shank and a flange to locate and secure the holder in a compatible machine-tool spindle. | Confirm that the holder, spindle interface, pull stud or clamping system, and machine control specification are compatible. |
| Applicable Standard | ISO 26623 defines polygonal taper interfaces for tool systems used with machine tools. The exact interface dimensions and tolerances must be taken from the applicable ISO 26623 part and machine documentation. | A supplier should provide drawings, dimensional inspection records, and clear confirmation of the relevant standard revision. |
| Taper Ratio | The PSC polygonal taper is commonly specified as 1:20. This indicates a 1 unit change in diameter over 20 units of axial length, subject to the standard’s dimensional definition. | The taper must match the spindle exactly. A similar-looking but non-matching taper can cause poor seating, vibration, or unsafe operation. |
| Polygonal Shank | The polygonal profile provides radial positioning and torque transmission through multiple contact surfaces rather than relying only on a round taper. | Consistent profile geometry and surface finish are essential for repeatable positioning, stiffness, and torque transfer. |
| Common Interface Sizes | PSC interface families commonly include nominal sizes such as PSC 32, PSC 40, PSC 50, PSC 63, PSC 80, and PSC 100. Availability and detailed dimensions depend on the applicable design and machine system. | Choose the size from the machine spindle specification rather than selecting only by cutting-tool diameter. |
| Tool Holding Options | Typical PSC configurations include milling holders, ER collet holders, hydraulic or shrink-fit holders, drill holders, boring holders, and face-milling adapters. | The holder type should match the cutter, required runout, gripping method, cutting load, coolant method, and available tool-change clearance. |
| Material Selection | Precision tool holders are commonly manufactured from alloy tool steel or other heat-treated steel grades selected for strength, dimensional stability, and wear resistance. | Request the material specification, heat-treatment condition, hardness range, and traceability documentation. |
| Balance Quality | Dynamic balance is normally expressed using ISO 21940 grades, such as G2.5 or G6.3, at a stated balancing speed. The required grade depends on tool geometry and operating speed. | A valid balance specification must include the grade, balancing speed, configuration, and maximum permitted operating speed. |
| Runout Performance | Runout depends on the holder type, measuring position, clamping system, gauge length, and tool diameter. It should be stated as a measured tolerance at a defined reference point. | Do not compare runout figures unless the measurement method and gauge length are identical. |
| Coolant Capability | PSC holders may be available with through-tool coolant, flange coolant, or external coolant arrangements, depending on the holder design and spindle system. | Verify pressure rating, coolant passage design, sealing method, and compatibility with the machine’s coolant delivery system. |
| Critical Inspection Points | Important checks include polygon taper dimensions, flange geometry, gauge length, concentricity, radial runout, key or drive features, thread accuracy, surface finish, and tool-clamping function. | Inspection should use calibrated equipment and documented acceptance criteria linked to the approved drawing. |
| Supplier Qualification | A capable supplier should demonstrate controlled machining, heat treatment, grinding, cleaning, final inspection, packaging, and batch traceability processes. | Evaluate quality records, inspection capability, production capacity, engineering support, lead time, export packaging, and after-sales response. |
| Recommended Purchasing Documents | Request a dimensioned drawing, material certificate, heat-treatment record, inspection report, balance report when applicable, runout result, surface-treatment details, and packaging specification. | Complete documentation reduces interface errors and supports incoming inspection and production traceability. |
Note: Exact dimensions, tolerances, permissible speeds, and clamping requirements should always be verified against the applicable ISO 26623 documentation, the machine-tool spindle specification, and the approved holder drawing.