How to Choose an FBE Coated LSAW Steel Pipe Factory
Selecting an FBE coated LSAW steel pipe factory takes more than comparing quotations. The pipe must match the project’s dimensions, steel grade, service conditions, and coating requirements. A low price means little if weld inspection records are incomplete or coating checks are unclear. Details matter.
Review how the factory controls each production stage. Ask how plate edges are prepared, seams are welded, and welds are inspected before coating. For the FBE process, check surface preparation, application conditions, coating thickness measurements, and holiday detection. Request sample inspection reports and confirm that pipe markings can be traced to production and test records. A clean workshop helps, but records show whether controls are consistent. Not always an easy distinction.
Factory capability should also fit your order. Ask about available pipe diameters, wall thicknesses, production capacity, inspection arrangements, and packing for transport. If possible, review a recent production batch or arrange an independent inspection. A smooth-looking coating sample may conceal uneven thickness, so visual checks alone are not enough. Compare the factory’s documented procedures with your project specification, and clarify who resolves nonconformities before production begins.
This guide explains practical ways to assess suppliers, verify quality evidence, and ask useful questions before placing an order. It also covers warning signs, communication, and delivery planning. No factory is right for every project. A careful choice of FBE coating LSAW steel pipe factory should rest on verified capability, clear documentation, and requirements agreed in writing.
Define the Project Requirements for FBE-Coated LSAW Steel Pipe
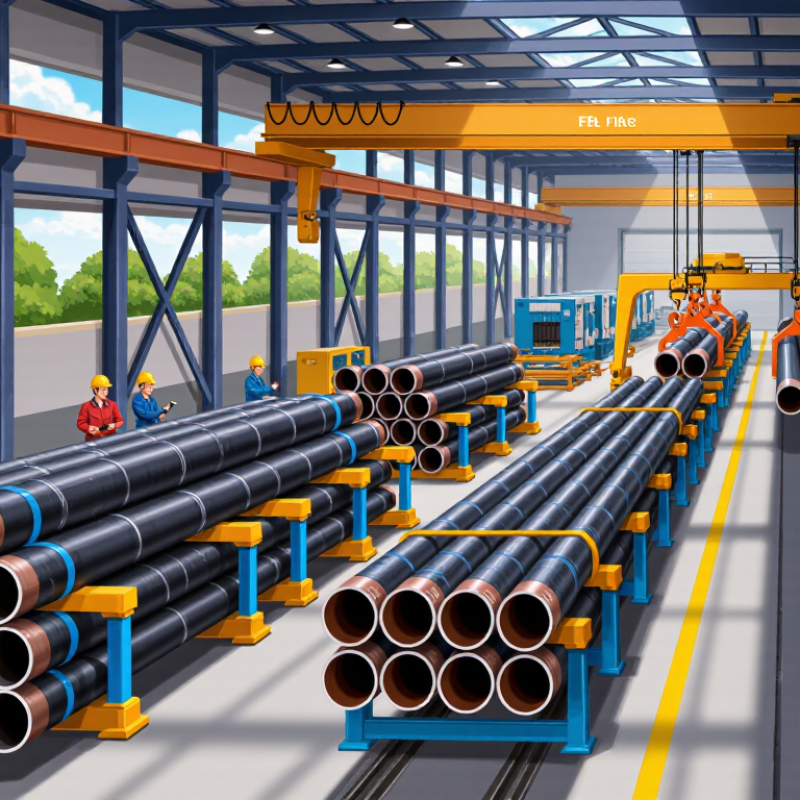
Before comparing an FBE-coated LSAW steel pipe factory, define the service conditions precisely. Record pipe diameter, wall thickness, steel grade, operating pressure, design temperature, and line length. Include soil resistivity, moisture, salinity, ultraviolet exposure, and installation method. These details influence coating selection and inspection depth.
ISO 21809-2 provides requirements for externally applied fusion-bonded epoxy coatings on line pipe. Your specification should identify the coating class, minimum dry-film thickness, surface preparation, curing range, adhesion, impact resistance, and allowable holiday limits. A common field target is about 350–500 micrometres, but the project engineer must confirm this range. Temperature matters. Poorly controlled curing can create weak adhesion beneath an attractive surface.
Ask factories for traceable batch records, steel mill certificates, calibration logs, and inspection results. Require test evidence for every production lot, not only laboratory samples. The NACE IMPACT study estimated global corrosion costs at approximately 3.4% of global GDP, showing why small specification gaps become expensive. API 5L requirements should also be matched with the project’s pressure and toughness needs. A clean document can still hide a poor assumption. Recheck transport damage, field joint coating, repair procedures, and cathodic protection compatibility before approving the purchase.
How to Choose an FBE Coated LSAW Steel Pipe Factory - Define the Project Requirements for FBE-Coated LSAW Steel Pipe
| Requirement | Illustrative Project Basis | What to Confirm with the Factory | Useful Records or Acceptance Evidence |
|---|---|---|---|
| Pipe application and service | Onshore transmission pipeline carrying natural gas; define operating conditions and design life in the project specification. | Confirm the factory can manufacture the required LSAW pipe and apply an external FBE coating suitable for the stated service and handling conditions. | Approved technical proposal, manufacturing procedure, and coating procedure linked to the project specification. |
| Pipe dimensions | Example: 610 mm outside diameter, 12.7 mm nominal wall thickness, and 12 m nominal length. These are sample values, not universal requirements. | Confirm the order schedule covers outside diameter, wall thickness, length, end preparation, tolerances, and any permitted dimensional range. | Dimension schedule, approved drawings, inspection and test plan, and dimensional inspection records. |
| Steel grade and product standard | Example: API 5L Grade X52, with the applicable product specification level stated in the purchase documents. | Verify that the mill can supply the specified grade and that material traceability is maintained from plate to finished pipe. | Material test certificates, heat-number traceability records, and required mechanical and chemical test results. |
| LSAW manufacturing requirements | Longitudinal submerged-arc-welded pipe; specify forming route, weld requirements, and inspection extent in the project documents. | Review the proposed forming and welding procedures, weld repair controls, and the required non-destructive examination coverage. | Welding procedure documentation, weld maps, NDT procedures, and examination reports required by the purchase specification. |
| External FBE coating standard | Specify the applicable coating standard and edition; ISO 21809-2 is a commonly referenced standard for external FBE coatings on pipeline transportation systems. | Confirm the factory's coating system, qualification basis, and inspection plan match the exact standard, edition, and project amendments. | Approved coating procedure, qualification records, and project-specific inspection and test plan. |
| Surface preparation | Define the required abrasive blast cleaning grade, surface profile, cleanliness, and soluble-salt limits in the project coating specification. | Ask how surface cleanliness and profile are measured, how often they are checked, and how prepared pipe is protected before coating. | Surface-preparation inspection logs, measurement records, and environmental condition records. |
| FBE coating thickness | Set the required minimum, target, and any maximum dry-film thickness in the purchase specification; the applicable requirement depends on the selected coating system and standard. | Confirm the factory can control and measure coating thickness across the pipe body and specified end areas. | Calibrated gauge records and thickness readings taken at the locations and frequency defined by the inspection plan. |
| Coating continuity and defects | Specify holiday detection voltage, inspection coverage, and the acceptance and repair rules using the applicable standard and coating thickness. | Confirm holiday testing is performed over the specified coated area and that repaired areas are re-inspected. | Holiday-test logs, repair records, and re-test results. |
| Adhesion and coating performance | State the required test methods, test temperature or conditioning, sampling frequency, and acceptance criteria in the project specification. | Check that testing uses the specified method and that test panels or pipe samples represent the production coating process. | Coating qualification test reports and production test results traceable to the relevant production lot. |
| Pipe ends and coating cutback | Define the uncoated end length, bevel geometry, and any temporary end protection required for welding and transport. | Confirm cutback consistency, end protection, and that coating does not interfere with the specified field-welding procedure. | End-dimension inspection records, packing details, and approved handling instructions. |
| Inspection and witness points | Identify hold points, witness points, document review, and inspection access for the purchaser or appointed inspector. | Confirm inspection notice periods, factory access, test equipment calibration, and how nonconformances are reported and closed. | Agreed inspection and test plan, calibration certificates, inspection reports, and nonconformance records. |
| Production capacity and delivery | State total quantity, lot sizes, required shipment dates, destination, and delivery sequence. | Check the proposed production schedule, coating-line capacity, storage arrangements, and shipping protection for coated pipe. | Production schedule, progress reports, packing list, and shipment inspection records. |
| Packaging, handling, and storage | Specify pipe stacking, separators, lifting method, weather protection, and storage duration or conditions where relevant. | Confirm handling practices minimize coating damage and that damaged coating is repaired and documented before dispatch. | Approved handling and packing procedure, visual inspection records, and repair documentation. |
| Final documentation and traceability | Define the required manufacturing data book contents, language, format, and submission timing. | Ensure pipe identification links each joint to its material heat, manufacturing records, inspection results, and coating batch. | Final data book, joint-by-joint traceability list, material certificates, NDT reports, coating test records, and release note. |
Note: The example dimensions and grade are illustrative only. Final values, test methods, coating criteria, and acceptance limits should be set by the project design basis, applicable standards, and purchase specification.